
Sand blasting (more uniform surface)
Removes floating powder and slight roughness to make the matte finish more consistent; suitable for assembly parts, structural parts and batch appearance consistency requirements.
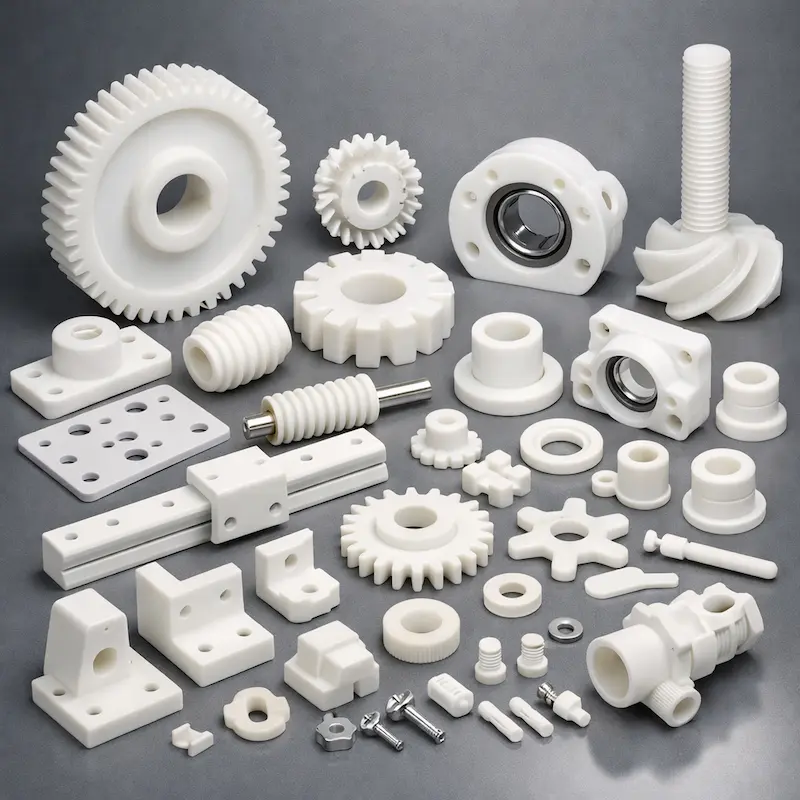
Nylon PA12-Solid White belongs to the SLS nylon system, leaning more toward a "functional" choice: balanced strength and toughness, abrasion and fatigue resistance, and no support required, suitable for complex structures and batch typesetting production.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | SLS selective laser sintering (PA12 nylon powder) |
|---|---|
| Color | White/natural color (typically fine matte texture; if you want a more uniform appearance, you can choose sandblasting/painting) |
| Layer thickness | 0.10–0.12 mm (common range, depending on equipment and layout strategy) |
| Dimensional tolerance | General reference ±0.20 mm or ±0.20% (whichever is greater); 2D tolerance or remark "Mate first" recommended for mounting holes/mating surfaces |
| Minimum wall thickness | ≥0.8 mm (recommended); ≥1.2–1.5 mm is recommended for slender/stressed areas; ≥2.0 mm is recommended near screws/buckles with fillets/reinforcements |
| Minimum aperture | Direct forming holes are recommended to be ≥1.5–2.0 mm; deep holes/long holes are recommended to be larger and powder discharge and secondary finishing are considered |
| Text/texture | The height of embossed characters is ≥0.5 mm; the depth of concave characters is ≥0.4 mm; the line width is ≥0.35–0.50 mm (painted parts are recommended to be larger) |
| Tensile strength | 45–55 MPa |
| Service temperature | About 120℃ (for short-term/working conditions, please evaluate based on actual usage requirements) |
| Density | About 1.02 g/cm³ |
| Surface texture | Fine matte, slightly grainy (powder sintering characteristics); sandblasting can be more uniform, and painting can achieve a more "finished" visual effect |
| Structural advantages | No support required, complex structure/inner buckle/porous array is more friendly; suitable for parallel typesetting of multiple pieces, conducive to low- to medium-volume production |
| Assembly enhancements | support Threaded inserts; Please indicate the thread specifications (such as M2/M3/M4), quantity and location; please note if enlarging/reaming is required |
| Finishing | Sandblasting, threaded inserts, and painting |
| Instructions for powder discharge | Closed cavities require design of powder vents/channels; complex inner cavities are recommended to undergo DFM in advance to avoid remaining powder affecting assembly and strength. |
| Typical lead time | Related to size, quantity, typesetting density and finishing; clear delivery and expedited options will be given after uploading the file |
Removes floating powder and slight roughness to make the matte finish more consistent; suitable for assembly parts, structural parts and batch appearance consistency requirements.
Used for screw connection and multiple disassembly and assembly; please indicate the thread specification, location and quantity in the remarks (please also indicate if enlarging/tapping is required).
It can be matte/semi-matte/high-gloss and other textures to enhance the display effect; it is recommended to provide reference pictures or color/texture targets.
It is suitable for structural validation, assembly parts and wear-resistant moving parts; it is more fatigue-resistant than resin and is more suitable for functional prototypes that can be installed and used.
It is easier to make inner buckles, grids, porous arrays, and complex shapes; it reduces support marks and finishing pressure, and is suitable for complex geometries.
Producing multiple pieces in the same furnace achieves better batch consistency; suitable for trial production, small batch spare parts, and multiple version iterations.
Supports sandblasting to improve consistency and painting to improve appearance. Threaded inserts Improve the reliability of screw assembly.
| Material | Key Advantages | Mainly applicable | Not suitable |
|---|---|---|---|
| Nylon PA12-Solid White | The functional type is more stable, does not require support, and is suitable for complex structures and low- to medium-volume typesetting. | Structural validation, assembly parts, wear-resistant moving parts, small batch functional parts | Ultimate mirror appearance, ultra-high precision fit (requires secondary processing/process change) |
| Black Nylon (SLS) | Both are functional types; the black appearance is more resistant to dirt and is suitable for functional parts with color requirements; | Assembly parts, structural parts, wear-resistant parts, batch functional parts | The ultimate mirror appearance and high-precision combination |
| HP Nylon - Gray (MJF) | Better batch consistency and dimensional stability, suitable for repeated delivery | Small and medium batch functional parts, assembly positioning parts, repetitive parts | Ultimate mirror appearance (still needs spray coating/finishing) |
| HP Nylon & Fiberglass - Black (MJF GF) | Stronger rigidity and dimensional stability, suitable for load-bearing structural parts/positioning parts | Load-bearing structural parts, assembly positioning parts, functional parts with priority on dimensional stability | Fasteners that require a certain degree of elasticity/toughness (needs evaluation) |
| Tough SLA - Yellow-Green (SLA) | A more refined appearance with greater detail; and more impact resistant than standard resins | Appearance + prototype with certain toughness, buckle verification, light load function verification | Complex structure mass layout, wear-resistant for long-term use (better with nylon) |
It is more of a "functional" choice and is often used for structural validation, assembly parts, wear-resistant moving parts and low- to medium-volume functional parts. Its advantages are concentrated in:
It is recommended to refer to the key requirements of drawing markings/remarks, and also refer to the parameter recommendations on this page:
If there are assembly mating/locating holes, it is strongly recommended to provide 2D annotations (PDF/DWG) for more accurate evaluation.
We support mainstream 3D/2D project files:
Faster and more accurate approach: priority delivery STEP + 2D annotation(Hole location/tolerance/fit requirements are clearer).
This is a typical surface feature of the powder sintering process. If you want a more delicate/unified appearance, common solutions:
Can be done, but must be considered Discharging powder:
You can directly indicate "whether opening of powder holes/location preference is allowed" in the remarks, and we will make DFM suggestions.
It is recommended to give priority to functional parts Threaded inserts:
If you need enlarging/reaming/tapping, please indicate it in the remarks and we will evaluate it according to the process route.
In addition to volume, SLS nylon quote is also affected by the following factors:
If it is a display piece, "sandblasting + painting" is recommended; if it is a functional piece, sandblasting is usually sufficient.
Both are functional nylon systems, and the main differences lie in appearance and usage preferences:
If you are going to spray paint, white is usually more friendly; if you want to "use the body color directly", you can choose according to your appearance preference.
Delivery time is related to size, quantity, typesetting density and finishing:
Expediting can be assessed, but it is recommended to clarify finishing and assembly requirements in advance to avoid rework affecting delivery.
In order to get a faster and more accurate quote, it is recommended to state the following when uploading the file:
Process: Upload drawings → Project evaluation and quote → Production and delivery after confirmation.