
Sand blasting (more uniform texture)
It is used to unify the matte graininess and touch of the surface and improve the consistency of appearance; it is more conducive to "consistent look and feel" for batch parts.
HP MJF Glass-Filled Nylon – Gray is based on HP MJF process, its advantages lie in "batch consistency" and "dimensional stability."
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
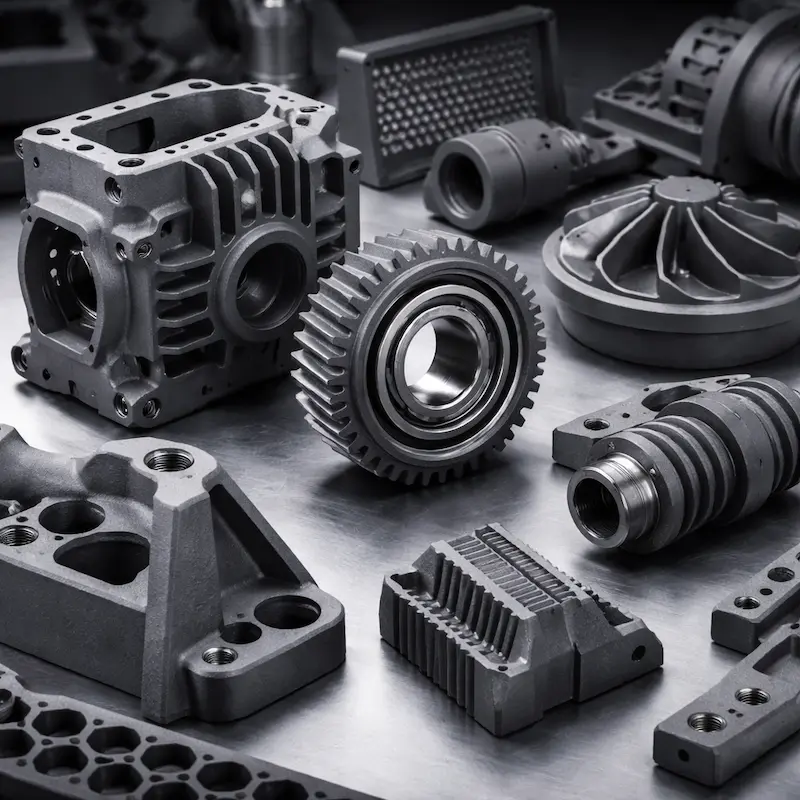
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | HP Multi Jet Fusion (MJF) 3D printing (glass fiber reinforced nylon) |
|---|---|
| Color | Gray (commonly used for engineering parts; more used for structural validation and positioning) |
| Dimensional tolerance | ±0.20 mm or ±0.20% (whichever is greater); it is recommended to mark the tolerance or note "accuracy first" for the key hole/datum surface |
| Minimum wall thickness | ≥0.8 mm (conventional); recommended ≥2.0 mm and reinforcement near load-bearing/screws |
| Rigidity and stability | Glass fiber reinforcement brings higher rigidity and lower warpage, suitable for positioning, support and load-bearing structures |
| Service temperature | About 150℃ (common indicators for materials; affected by working conditions and design) |
| Tensile strength | 60–80 MPa (glass fiber reinforced version is more strength/rigid oriented) |
| Density | About 1.02 g/cm³ |
| Assembly enhancements | support Threaded inserts;Please indicate the thread specification (such as M2/M3/M4), quantity and location; If you need to enlarge/ream/tapping, please make a note (for more stable assembly accuracy) |
| Finishing | Sandblasting, threaded inserts, and painting |
| Typical lead time | Related to size, quantity, typesetting density and finishing; clear delivery and expedited options will be given after uploading the file |
It is used to unify the matte graininess and touch of the surface and improve the consistency of appearance; it is more conducive to "consistent look and feel" for batch parts.
When you need uniform color, covering powder texture, or a more "finished" display effect, you can choose painting; it is recommended to provide reference pictures or texture requirements (matte/semi-matte).
Suitable for structural parts that require repeated disassembly and assembly of screws, positioning and fastening, or load-bearing connections; please note the thread specifications, quantity, and location (secondary processing of the hole location can be evaluated if necessary).
Glass fiber reinforcement improves rigidity and is more suitable for support, positioning, and load-bearing structures; it is more friendly to structural parts that are more sensitive to deformation.
Suitable for delivery of low- to medium-volume production of repetitive parts, assembling positioning parts and fixture parts; more controllable dimensional fluctuations in parallel production of multiple parts.
Compared with SLA resin which is partial to appearance, it is more suitable for long-term structural validation and assembly reliability evaluation; it can be used as a "functional validation material" before mass production.
support Threaded inserts Improve the reliability of screw connections; with sandblasting/painting, you can achieve a better balance between function and appearance.
| Material | Key Advantages | Mainly applicable | Not suitable |
|---|---|---|---|
| HP Nylon - Gray (MJF) | Batch consistency and dimensional stability ensure more stable delivery of functional parts | Delivery of low- to medium-volume production of functional parts, assemblies, and repetitive parts | A higher rigidity load-bearing positioning structure is required (GF version is better) |
| HP Nylon & Fiberglass - Black (MJF GF) | High rigidity and dimensional stability, suitable for load-bearing structures and positioning parts | Priority is given to load-bearing structural parts, assembly positioning parts, and dimensional stability. | Fasteners that require elasticity/toughness (needs evaluation) |
| White Nylon (SLS) | Strong and balanced, no support required, suitable for complex structures and typesetting production | Structural validation, assembly parts, wear-resistant moving parts, small batch functional parts | Ultimate mirror appearance, ultra-high precision fit (requires secondary processing/process change) |
| Black Nylon (SLS) | The functional type is more stable, black is more resistant to dirt, and is suitable for functional parts with color requirements. | Assembly parts, structural parts, wear-resistant parts, batch functional parts | The ultimate mirror appearance and high-precision combination |
| Tough SLA - Yellow-Green (SLA) | A more refined appearance with greater detail; and more impact resistant than standard resins | Appearance + prototype with certain toughness, buckle verification, light load function verification | Complex structure mass layout, wear-resistant for long-term use (better with nylon) |
It prefers "structure and stability first" and is often used for the delivery of load-bearing structural parts, assembly positioning parts and small and medium-sized repetitive parts. Its advantages are concentrated in:
Glass fiber reinforcement is more "rigid and stable", so you need to be cautious in structures that require elasticity and fatigue life:
It is recommended to refer to the key requirements in your drawings/notes; at the same time, you can refer to the commonly used ordering indicators for materials:
For positioning holes/assembly holes: It is recommended to provide 2D annotations (PDF/DWG) and note "key holes/key surfaces". If necessary, secondary reaming/reaming and threaded inserts options can be evaluated.
We support mainstream 3D/2D project files:
Faster and more accurate advice: Prioritized STEP + 2D annotation, and mark the key hole locations, tolerances and assembly benchmarks.
MJF GF quote not only depends on volume, but also is affected by the following factors:
If you want to get a quote that is closer to your target, it is recommended to note: Purpose (load bearing/positioning/assembly) + quantity + critical dimensions/tolerances + finishing requirements + lead time.
Common finishing of this material (consistent with the material library):
If you are pursuing finished product effects, it is recommended to note: Target texture (matte/semi-matte) + reference image + key appearance surface.
Very suitable for assembly positioning and structure verification, but it is recommended to use an "engineering order placement method" to improve reliability:
The lead time is related to the size, quantity, typesetting density and finishing; after uploading the file, a clear lead time and expedited option will be given.
Expediting can be assessed, but it is recommended to clarify in advance: Critical dimensions/inspection methods + finishing scope + appearance standards, to avoid rework affecting the overall cycle.
In order to get a faster and more accurate quote, it is recommended that you provide/explain when uploading the file:
You only need three steps: Upload drawings → Confirm project evaluation and quote → Production and delivery after confirmation.