
chamfer
Used to remove sharp edges and improve assembly feel and safety; it is recommended to specify the chamfer size and position for sliding/rotating fittings.
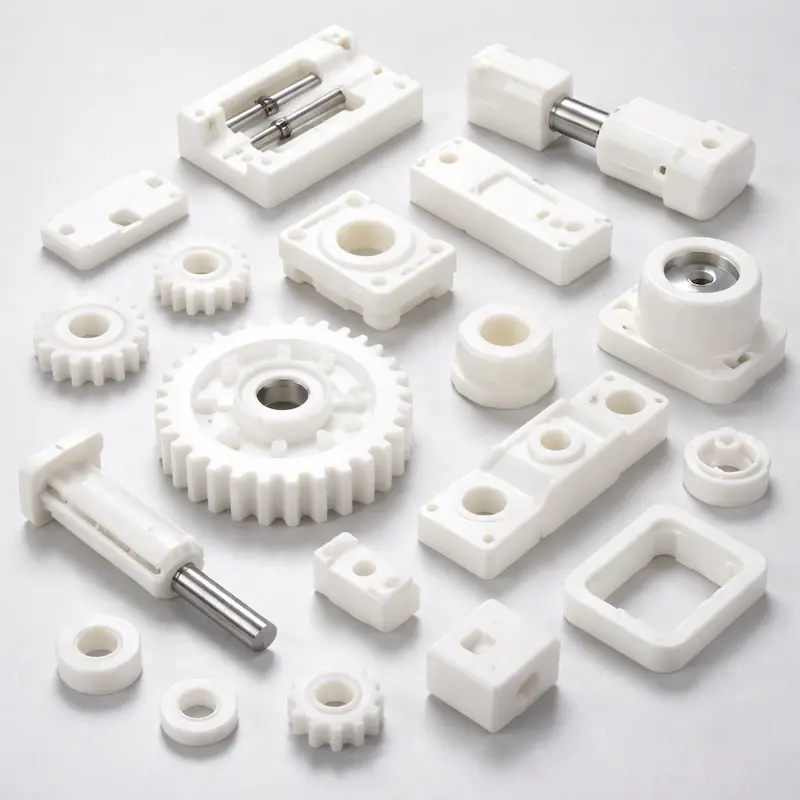
Acetal (POM) effect resin is mainly used in vacuum casting for functional verification parts with "low friction / high dimensional stability."
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | Vacuum casting (silicone mold + PU vacuum casting, POM simulation) |
|---|---|
| Material positioning | Low-friction/wear-resistant guide small-batch functional prototypes and assembly verification solutions |
| Accuracy | Conventional ±0.30 mm or ±0.30% (whichever is greater); 2D tolerance marking is recommended for critical mating surfaces |
| Minimum wall thickness | Recommended ≥1.0 mm; recommended ≥1.5–2.0 mm near force/screws (depending on structural evaluation) |
| Minimum aperture | Recommended ≥1.8–2.0 mm; it is recommended to reserve a margin for the mating hole and re-expand/ream the hole |
| Service temperature | Reference range -40~100℃ (related to resin system/post-curing; please specify in advance for continuous high temperature) |
| Strength (tensile strength) | Reference range 50–70 MPa (depends on resin system/working conditions) |
| Density | Reference approx. 1.35–1.45 g/cm³ |
| Appearance and color | Common natural colors (white/off-white) are mainly used; if you need to specify a color/matching color, please make a note and provide a reference color |
| Typical structures suitable for | Gears, sliders, bushings, positioning parts, mechanism components (emphasis on low friction and wear-resistant feel) |
| Not recommended scenario | Long-term high temperature, long-term heavy load wear, strong impact/high fatigue (it is recommended to change materials or processes) |
| Finishing | Chamfering, grinding, bonding, screen printing, laser engraving |
| Typical lead time | Related to size, quantity, mold opening complexity and finishing; clear delivery and expedited options will be given after uploading the file |
Used to remove sharp edges and improve assembly feel and safety; it is recommended to specify the chamfer size and position for sliding/rotating fittings.
Used to improve parting lines, gate areas and surface details; if the appearance surface is sensitive, it is recommended to define the display surface and appearance standards in the remarks.
Suitable for assembly and assembly verification of component structures; it is recommended to reserve positioning structures (tongues/positioning posts) to improve assembly consistency.
Suitable for logos, scales and other flat graphic information; it is recommended to provide vector files and location and size instructions.
For permanent identification (serial number/QR code/Logo); please provide engraving content, location and depth requirements.
Finishing items are subject to material data: chamfering, grinding, bonding, screen printing, laser engraving.
It is closer to the mechanical experience of engineering plastics and is suitable for feel evaluation and linkage verification of sliding/rotating structures.
Suitable for short-cycle functional validation of gears, sliders, bushings and other structures (long-term heavy loads require the evaluation of more secure routes).
Compared with injection molding, it enters the verification stage faster and is suitable for iteration and trial production needs of about 5-200 pieces.
Supports screen printing/laser engraving and bonding assembly, which facilitates version differentiation, assembly demonstration and small batch delivery.
Polyoxymethylene-POM (vacuum-cast parts mold) is mainly used for small batch functional prototypes and assembly verification. Its advantages are concentrated in:
Vacuum casting uses silicone mold + PU resin casting to "simulate" the feel and functional characteristics of POM, but it is still different from injection molding:
It is recommended to refer to the key requirements of drawings and notes. Common references:
It is recommended to provide both 3D + 2D (if there are tolerance/fit requirements):
Yes. It is recommended to include positioning structures in the design to improve consistency:
Supported finishing projects are: chamfering, grinding, bonding, screen printing, and laser engraving.
When identification such as logo/serial number/QR code is required, priority is given to suggestions Laser engraving(permanent) or screen printing(More visually striking).
After uploading the file, we will provide feedback with quote and manufacturability suggestions (DFM) as soon as possible, and provide more suitable parting/pouring and finishing solutions.