
heat treatment
Used to improve comprehensive properties such as strength, toughness and wear resistance. If there is a target hardness/condition, please write it down in the order notes.
40Cr is a classic alloy structural steel, with advantages such as "high strength, good toughness, and more stable fatigue performance after quenching and tempering," suitable for functional parts that bear loads, withstand impact, and require longer service life.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | CNC Machining |
|---|---|
| Material grade | Alloy steel 40Cr (alloy structural steel) |
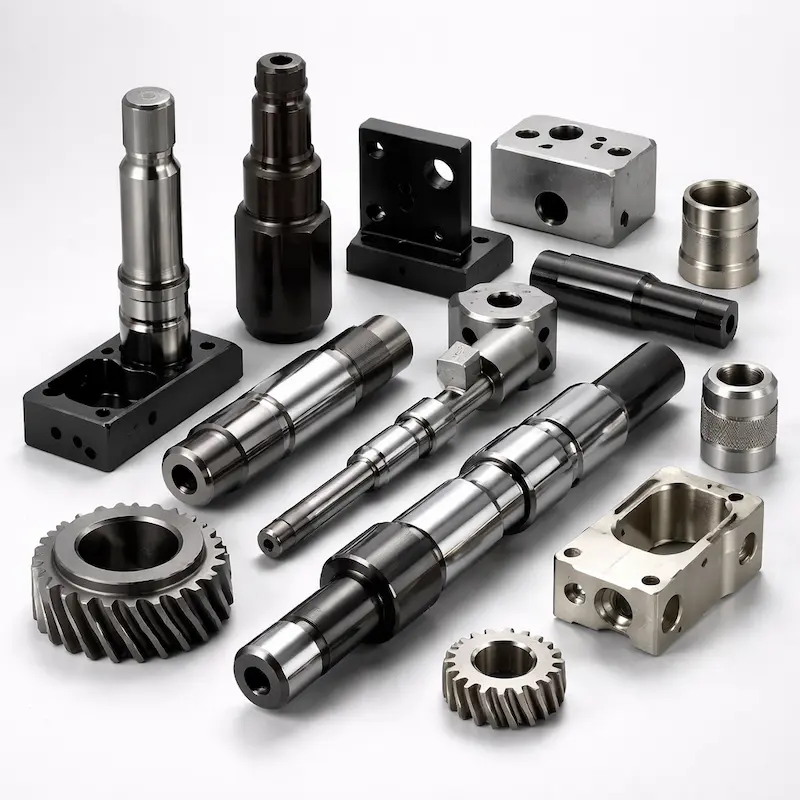
| Applications | Small batch processing of load-bearing structural parts, shafts, gears, connectors and high-load functional parts |
| Machining tolerance | ±0.2 mm |
| Minimum wall thickness | 1.0mm |
| Service temperature | 300-600℃ |
| Tensile strength | 450-1100MPa |
| Density | 7.7-8.5 g/cm³ |
| Heat treatment recommendations | If you need higher strength/wear resistance/fatigue life, it is recommended to describe the target performance and usage conditions in the remarks. Engineers can recommend appropriate heat treatment routes and processing sequences. |
| Finishing | Heat treatment, sand blasting, blackening, oxidation, nickel plating, chrome plating |
| Typical lead time | Related to structural complexity, tolerances, heat treatment and surface finishing options; clear lead time and expedited feasibility will be given after uploading the file |
Used to improve comprehensive properties such as strength, toughness and wear resistance. If there is a target hardness/condition, please write it down in the order notes.
It is used to unify the surface texture and reduce the visibility of knife marks, and also facilitates the consistency of subsequent surface treatments.
It is often used for surface rust prevention and appearance treatment of steel parts; it is recommended to provide reference when you are sensitive to color consistency and appearance standards.
Used to improve surface corrosion resistance and appearance consistency; if you require a specific appearance or corrosion resistance target, please indicate it in the remarks.
Used to improve corrosion resistance and surface hardness/wear resistance; suitable for parts that require both appearance and corrosion resistance.
Used to improve surface wear resistance, corrosion resistance and appearance brightness; if it is a mating surface/sliding surface, please mark the key dimensions and coating requirements.
Suitable for load-bearing, impact-bearing and functional parts requiring higher fatigue life, it is a common choice for upgrading from ordinary carbon steel.
The overall performance can be improved through the heat treatment route; it is more friendly to high-load structural parts.
It is common in transmission and load-bearing scenarios; it is easier to achieve stable assembly results by cooperating with drawing tolerances and DFM review.
Supports sandblasting, blackening, oxidation, nickel plating, chromium plating and other solutions to facilitate the balance between corrosion resistance and appearance.
Alloy steel 40Cr is more suitable for high strength/high toughness structural requirements and is commonly used in load-bearing structural parts, shafts, gears, connectors and other high-load functional parts. The advantage is that strength and toughness are more balanced, and it can be combined with heat treatment to further enhance overall performance.
It is recommended to provide 3D + 2D markings for faster and more accurate quote:
You can first click on the common references in the material library:
If there are key assembly holes/mating surfaces, please mark the key requirements in the 2D drawing or remarks, and we will conduct a DFM assessment based on the drawings and structure.
Heat treatment can be used to improve comprehensive properties such as strength, toughness and wear resistance, and is suitable for parts with higher load-bearing and fatigue life requirements. Suggested remarks:
The finishing of alloy steel 40Cr provides the following options according to the material library:
If your goal is to prioritize rust prevention, you can give priority to blackening/oxidation/nickel plating; if you pay attention to both wear resistance and appearance brightness, you can evaluate chrome plating. It is recommended to describe the use environment and appearance standards in the remarks.
Quotes are usually more affected by the following factors:
Recommended practices include:
If the mating surface/hole position is sensitive to size, it is recommended to specify it in the 2D drawing:
This will help us plan processing allowances and inspection strategies and reduce the risk of rework.
If you pay more attention to strength/toughness and load-load-bearing capacity, and can solve rust prevention through surface finishing, alloy steel 40Cr is usually more suitable; if your use environment requires higher corrosion resistance (humidity/salt spray/chemical media), it is recommended to prioritize the evaluation of stainless steel systems.
It is recommended to provide/explain when uploading the file:
After submission, we will provide a quote, lead time and manufacturability suggestion (DFM) simultaneously.