
chamfer
Used to remove sharp edges and improve assembly feel and safety; it also helps reduce the risk of edge chipping and stress concentration.
ABS(acrylonitrile-butadiene-styrene copolymer) is one of the most commonly used engineering plastics in injection molding, featuring excellent overall mechanical properties, dimensional stability, and processing fluidity.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
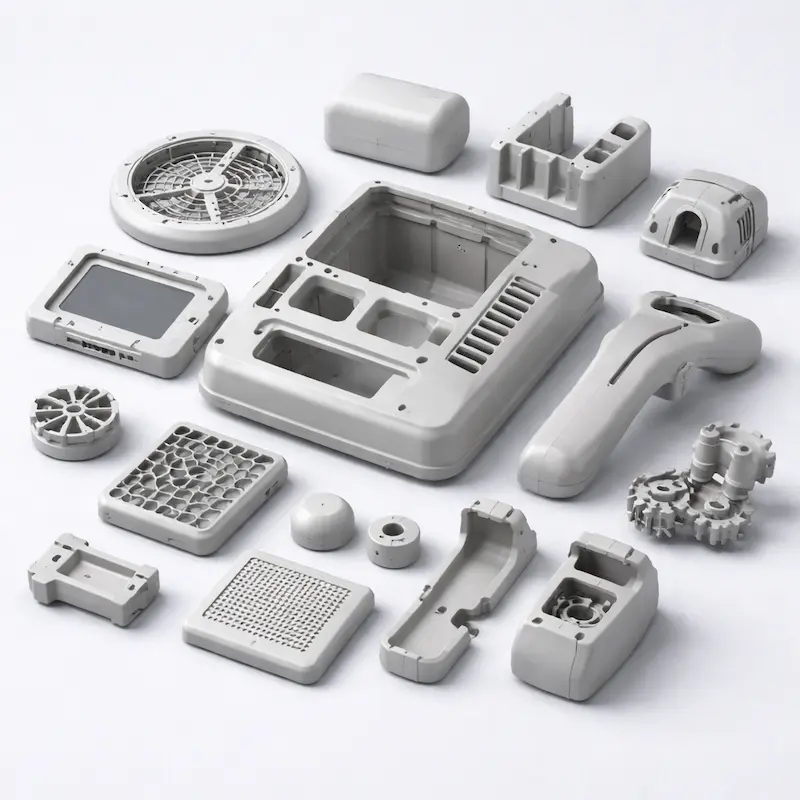
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | Injection Molding |
|---|---|
| Material | ABS |
| Material overview | ABS is a common material option in injection molding scenarios, suitable for balancing cost, appearance and performance. |
| Applications | Suitable for scenarios such as prototypes and functional validation, you can choose a more suitable material solution based on appearance, strength, temperature resistance and cost targets. |
| Accuracy | ±0.2 mm |
| Minimum wall thickness | 1.0mm |
| Service temperature | 300-600℃ |
| Tensile strength | 450-1100MPa |
| Density | 7.7-8.5 g/cm³ |
| Finishing | Chamfering, grinding, bonding, screen printing, laser engraving |
| Typical lead time | Related to structure, quantity, mold/tooling plan and finishing; clear delivery and expedited options will be given after uploading the file |
Used to remove sharp edges and improve assembly feel and safety; it also helps reduce the risk of edge chipping and stress concentration.
Used to optimize the touch and details of the appearance surface; suitable for injection molded parts that require appearance consistency and feel.
Suitable for component structure or assembly needs; it is recommended to reserve the bonding surface and positioning structure during the design stage, and explain the bonding strength/appearance requirements in the remarks.
Used for graphic information such as logos, marks, and scales; it is recommended to provide vector files and position and size instructions to ensure consistency and testability.
Suitable for serial numbers, QR codes and durable markings; it is recommended to reserve a flat craft surface and clarify font size/depth and contrast requirements.
Injection molding enables stable, repeatable manufacturing; when you need plastic parts for volume delivery, ABS is a common starting point.
Suitable for low-cost general-purpose parts, achieving a more controllable balance between appearance, structure and delivery efficiency.
Suitable for structural parts/shell designs that require electrical insulation (specific indicators can be noted when enquiring).
Supports chamfering, grinding, bonding, screen printing, laser engraving and other processing, making it easier to meet marking and assembly needs.
ABS is commonly used for general plastic parts, shell parts and functional validation samples. Its advantages are usually reflected in:
You can refer to the parameter range on this page:
If there are assembly holes, positioning surfaces or tight tolerance fits, it is recommended to provide 2D markings and key dimension descriptions, and we will conduct a DFM assessment based on your assembly goals.
Faster and more accurate way: STEP + 2D tolerance marking, and note the appearance and assembly requirements.
ABS supported finishing includes: Chamfering, grinding, bonding, screen printing, laser engraving.
It is recommended to write clearly in the inquiry remarks: bonding location, strength requirements and appearance standards.
You only need three steps: Upload drawings → Confirm project evaluation and quote → Production and delivery after confirmation.